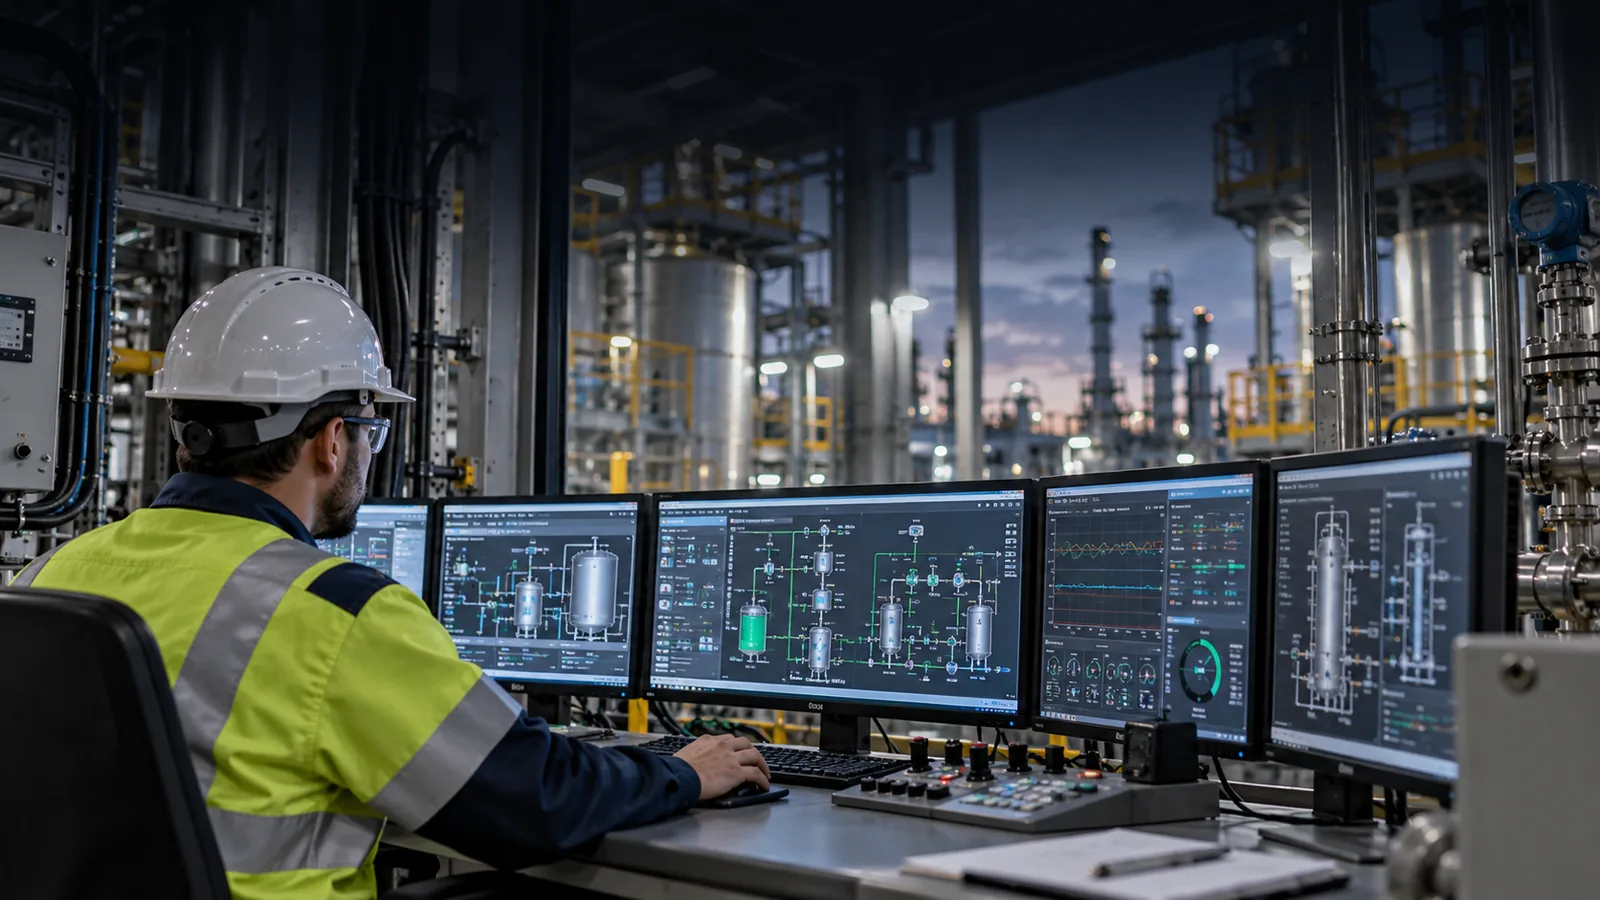
Alarms are intended to warn operators when a process condition requires attention.
A high pressure, rising temperature, equipment trip or loss of utility may all generate an alarm in the control room.
When designed well, alarms help operators recognise abnormal situations and respond before the condition becomes more serious.
But when too many alarms appear at once, the alarm system can become part of the problem.
Not every process change needs an alarm.
An effective alarm should indicate a condition that requires the operator to recognise the situation and take some form of action.
If no action is expected, the information may be better displayed as a status message, event or trend rather than an alarm.
This distinction is important because every unnecessary alarm adds to the operator’s workload.
Over time, poorly selected alarms can make the system crowded and difficult to use.
A control room may contain thousands of configured alarm points.
If many of these activate frequently, operators can become accustomed to constant alarm activity.
Nuisance alarms may appear repeatedly even when no meaningful action is required.
Other alarms may remain active for long periods.
When the alarm system becomes noisy, important signals can be harder to recognise.
The result is a paradox: more alarms can create less useful information.
An alarm flood occurs when many alarms arrive within a short period.
This often happens during a process disturbance, equipment trip or utility failure.
A single initiating event can trigger a chain of secondary alarms.
For example, the trip of one major piece of equipment may cause changes in flow, pressure, level and temperature across several systems.
The operator may then receive dozens or hundreds of alarms even though many originate from the same underlying event.
The challenge is identifying which alarms matter first.
Alarm priority indicates how urgently the operator needs to respond.
Plants commonly use several priority levels.
The highest priorities should be reserved for conditions with significant consequences and limited response time.
If too many alarms are classified as high priority, the priority system loses its purpose.
Effective prioritisation considers factors such as:
Priority should help guide attention rather than simply indicate that something is important.
Alarm rationalisation is the process of reviewing individual alarms and deciding whether each one is necessary and how it should behave.
The review typically considers:
This process helps remove duplicates and alarms that do not lead to useful operator action.
It also creates clearer documentation for the remaining alarms.
Alarm limits should be far enough from normal operating conditions to avoid unnecessary activation but early enough to give operators time to respond.
If a high-level alarm is set too close to the normal operating level, routine fluctuations may trigger repeated alarms.
If it is set too close to a trip point, the operator may have very little time to act.
Alarm settings therefore need to reflect the actual operating envelope and response time available.
Some process values fluctuate around an alarm limit.
This can cause an alarm to repeatedly activate and clear.
The result is often called alarm chattering.
Deadband can reduce this problem by requiring the process value to move a defined distance away from the alarm limit before the alarm clears.
Time delays can also help prevent short-lived process fluctuations from creating unnecessary alarms.
These features need to be applied carefully so that genuine abnormal conditions are not hidden.
A standing alarm is one that remains active for an extended period.
Some standing alarms may reflect known equipment conditions or temporarily unavailable systems.
But large numbers of persistent alarms can clutter the alarm display.
Operators may begin to ignore them.
Regular review helps determine whether the alarm remains valid, whether the underlying issue should be corrected or whether the alarm configuration itself needs to change.
Modern control systems may allow operators to temporarily shelve an alarm.
This can be useful when a known condition is generating repeated alarms while maintenance is being carried out.
But shelving needs clear rules.
If alarms remain hidden without appropriate control, a real process risk can be overlooked.
Shelved alarms should therefore be visible, time-limited where appropriate and periodically reviewed.
Alarm management should not stop once the system is configured.
Plants can monitor how the alarm system actually performs.
Useful indicators may include:
These measures help identify where the alarm system is creating unnecessary workload.
An alarm tells the operator that something requires attention, but it should also be clear what that attention means.
For significant alarms, operating procedures or alarm-response guidance may define:
This becomes particularly valuable during abnormal situations when operators need to make decisions quickly.
Industrial plants change over time.
Equipment is modified, operating conditions change and new control logic is introduced.
Alarm systems need to evolve with those changes.
An alarm configuration that was appropriate when the plant was commissioned may no longer reflect the current process.
Management of change should therefore consider alarm impacts whenever equipment or process conditions are modified.
Operators rely on alarms most heavily when the plant is no longer behaving normally.
That is precisely when clear information is most important.
A well-managed alarm system helps operators identify significant conditions, understand their priority and respond in time.
A poorly managed system can overwhelm the same operators with information when they are already under pressure.
For industrial plants, good alarm management is therefore not about creating more alarms.
It is about ensuring that the alarms that remain are meaningful, actionable and useful when the plant needs them most.